İnşaattan sorumluyuz----- üretimden sorumluyuz----- eğitimden sorumluyuz

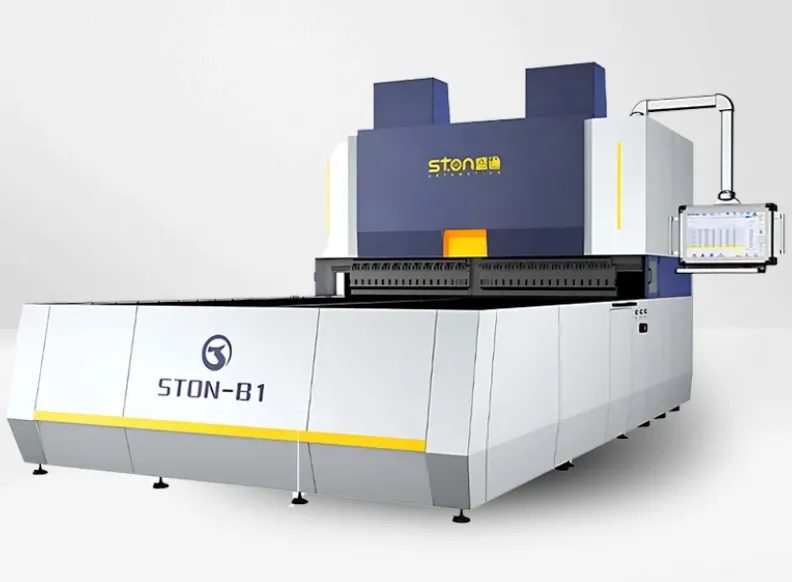
A server rack bending machine forms 19-inch rack frames and mounting rails from cold-rolled or stainless sheet, using CNC panel bending and turret punching to hold rack-frame diagonal squareness and mounting-hole pitch within a tight, repeatable band — the number that decides whether 42U of rail brackets line up without shimming.
A 19-inch rack isn’t tolerant the way a filing cabinet is. The EIA-310 hole pattern on the mounting rails has to repeat down the full height of the frame — 18U, 42U, whatever the customer ordered — and every panel that bolts to it has to land on those holes without forcing. Three things stack up against you:
Get any one of these wrong by a small amount and it doesn’t show up on a single panel — it shows up as accumulated drift once you’re bolting a dozen pieces into one cabinet. That’s tolerance stack-up, and it’s the actual failure mode rack fabricators run into, not “the metal doesn’t bend.”
STON’s published parameters for the equipment that covers this workflow — blank preparation, panel bending, and hole punching — are below. These come from STON’s own production-line and machine documentation, not general industry averages.
| Process Stage | Parametre | Specification | Source |
|---|---|---|---|
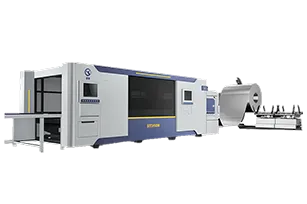
| Uncoiling & Leveling (Blank Preparation) | Diyagonal Doğruluk | ≤1 mm / 2000 mm | STON Uncoiling-Leveling-Laser Cutting Production Line |
| Uncoiling & Leveling (Blank Preparation) | Tesviye Doğruluğu | ±1 mm / m² | STON Uncoiling-Leveling-Laser Cutting Production Line |
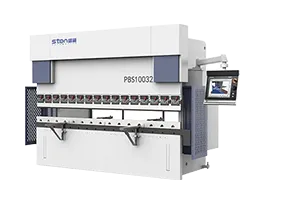
| Panel Bending (Vacuum/Suction Type) | Angle Accuracy | Yaklaşık ±0,5°/m | STON Suction Cup Type Panel Bender, Common Parameters |
| Panel Bending (Vacuum/Suction Type) | Dimensional Accuracy | Approx. ±0.1 mm/m | STON Suction Cup Type Panel Bender, Common Parameters |
| Panel Bending (Vacuum/Suction Type) | Düzlük | Approx. 0.2 mm/m | STON Suction Cup Type Panel Bender, Common Parameters |
| Turret Punching (Servo) | Machining Accuracy | ±0,1 mm | STON Servo CNC Turret Punching Machine |
| Turret Punching (Servo) | Maximum Load Capacity | 150 kg | STON Servo CNC Turret Punching Machine |
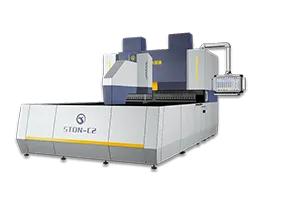
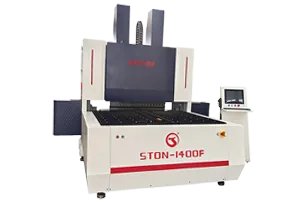
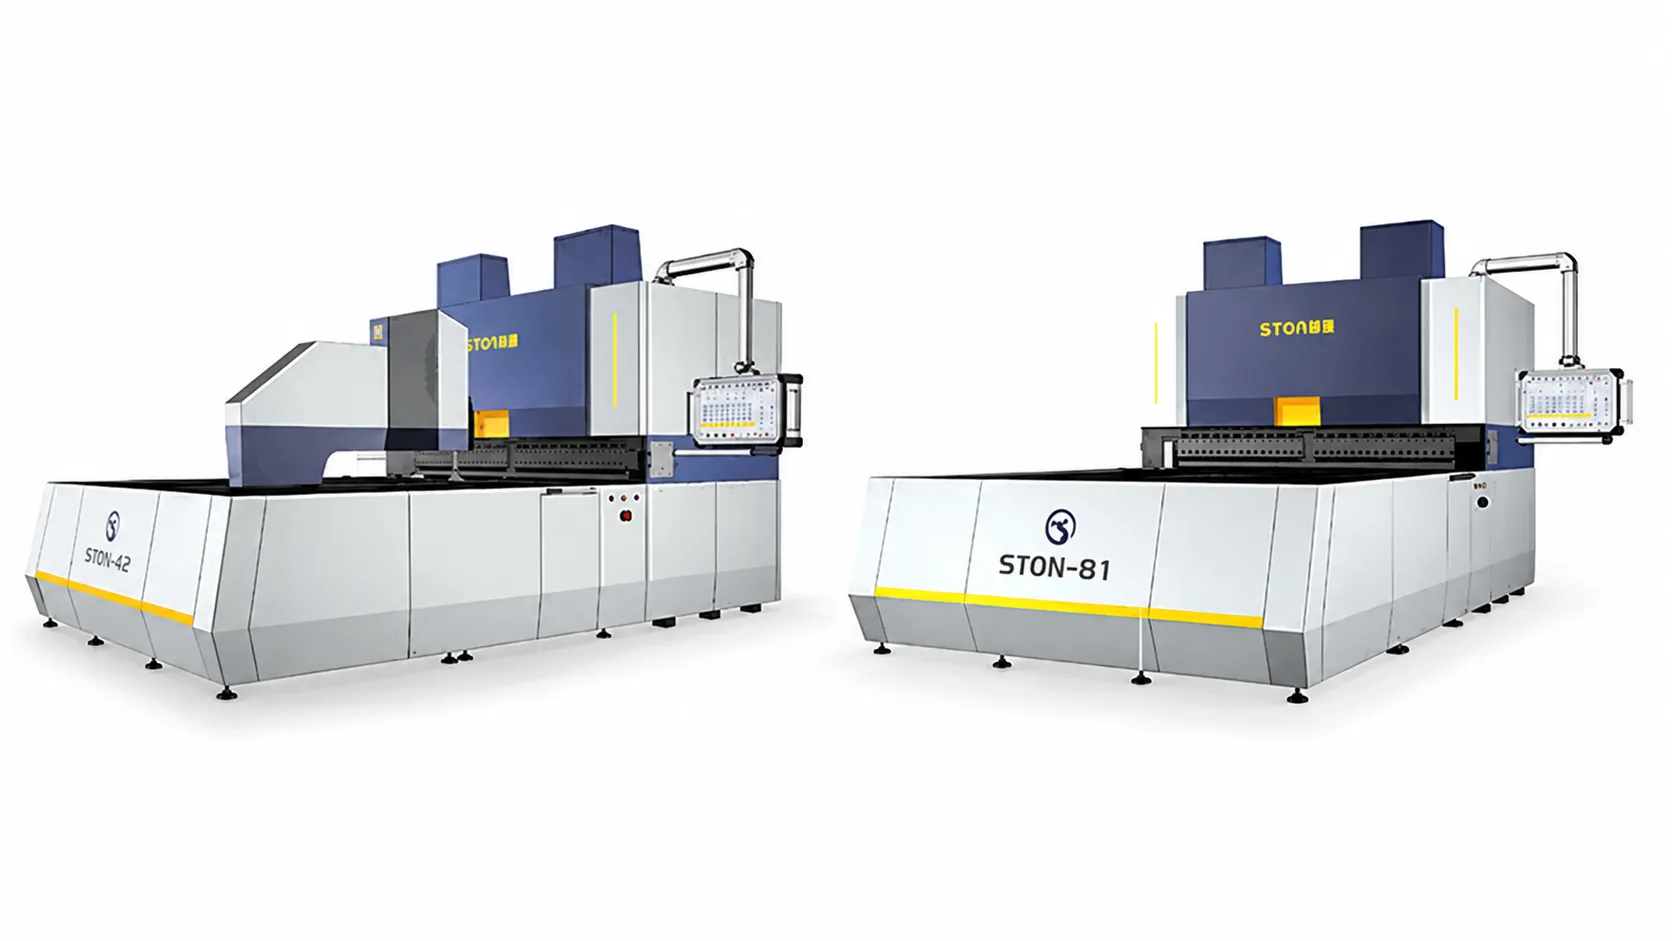
Rack panels typically run 1.0–2.0 mm cold-rolled or 1.0–1.5 mm stainless — light enough that most panel bender frame sizes handle it, but the bed construction still matters. STON’s Press Arm Type panel bender comes in welded-bed and cast-bed versions, and the two are not interchangeable on thickness:
| Process Stage | Parametre | Specification | Source |
|---|---|---|---|
| Uncoiling & Leveling (Blank Preparation) | Diyagonal Doğruluk | ≤1 mm / 2000 mm | STON Uncoiling-Leveling-Laser Cutting Production Line |
| Uncoiling & Leveling (Blank Preparation) | Tesviye Doğruluğu | ±1 mm / m² | STON Uncoiling-Leveling-Laser Cutting Production Line |
| Panel Bending (Vacuum/Suction Type) | Angle Accuracy | Yaklaşık ±0,5°/m | STON Suction Cup Type Panel Bender, Common Parameters |
| Panel Bending (Vacuum/Suction Type) | Dimensional Accuracy | Approx. ±0.1 mm/m | STON Suction Cup Type Panel Bender, Common Parameters |
| Panel Bending (Vacuum/Suction Type) | Düzlük | Approx. 0.2 mm/m | STON Suction Cup Type Panel Bender, Common Parameters |
| Turret Punching (Servo) | Machining Accuracy | ±0,1 mm | STON Servo CNC Turret Punching Machine |
| Turret Punching (Servo) | Maximum Load Capacity | 150 kg | STON Servo CNC Turret Punching Machine |
For a 600–800 mm deep, 42U-tall rack frame, the 1400 or 1600 frame size covers the side panels and rear doors in one setup; going to a 2000 or 2500 frame only matters if you’re bending full-height single-piece side rails rather than joining sections. The bending height range (170/300/400 mm) is worth checking against your deepest flange — a 42U frame with a full-depth base pan can push past the shallow setting.

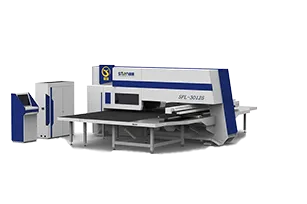
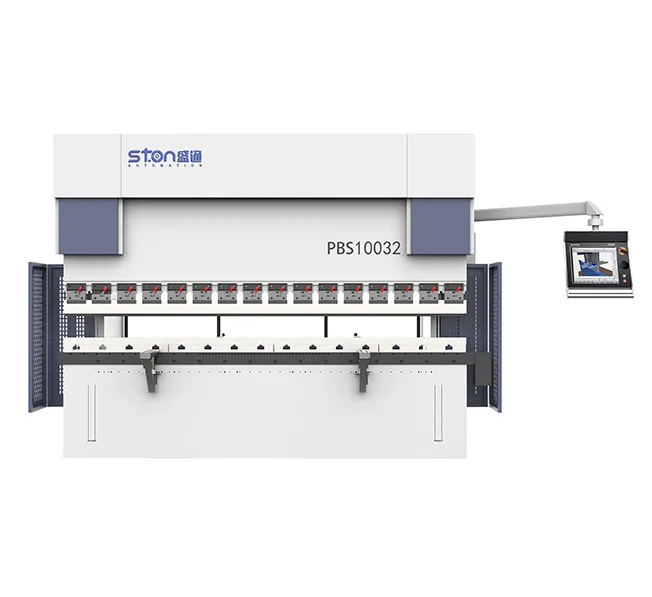
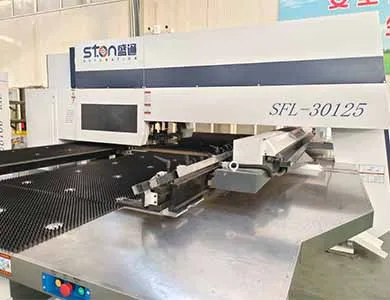
Panel benders form the fold lines; they don’t put the EIA-310 mounting holes in the rail. That’s the turret punch’s job, and it’s why the recommended pairing for rack-frame production is a panel bender plus a servo CNC taret zımba presi rather than the bender alone. STON’s servo turret punch holds ±0.1 mm machining accuracy at up to 150 kg part load, with independent control of two rotary stations for angled or slotted hole patterns — relevant for cage-nut cutouts and cable pass-throughs that aren’t simple round holes.
Compared with a shared punch-press setup running multiple part families off one turret without dedicated rack tooling, a line sized specifically for rack-rail hole spacing avoids re-indexing the turret between runs, which is where pitch drift tends to creep in on high-mix production.

The combination above holds tolerance through bending and punching. It does not compensate for a bad blank — if the incoming coil or sheet isn’t flat within the leveling line’s own ±1 mm/m² spec, no amount of bending accuracy downstream recovers squareness. It also doesn’t include welding: rack frames that need corner welds for extra rigidity add a separate process and its own heat-distortion risk, which isn’t covered by the bending and punching figures above. And the automatic tool-change and C-axis lifting options that speed up mixed rack-size production are configurable additions, not standard on the base panel bender — specify them up front, since retrofitting later means a longer lead time than ordering with the machine.
Pricing depends on frame size, bed type (welded vs. cast), axis count, and tooling package. Buyers should request a quote against their actual rack dimensions and material spec rather than working from a general figure.
Usually yes for a 1400 or 1600 frame size, since rack panels rarely exceed 1250 mm in the constrained bend dimension. Confirm against your deepest cabinet, since depth plus flange allowance can push close to the frame limit.
No — that figure is published for STON’s uncoiling and leveling line, which prepares the flat blank before bending. The panel bender’s own accuracy is separately specified as angle accuracy (~±0.5°/m) and dimensional accuracy (~±0.1 mm/m).
STON’s panel bender line doesn’t list an integrated punching add-on in current documentation. For EIA-310 hole patterns, a dedicated turret punch press is the documented path.
İster mevcut bir hattı geliştiriyor ister yeni bir projeye başlıyor olun, STON üretiminiz için bir CNC çözümünü özelleştirecektir.